OEM Tubular Steel Towers in China: Precision Manufacturing for Stronger Networks
2026-11-02
Behind every strong network is a tower built with more than just steel—it's built with precision that most never see. In China's OEM manufacturing scene, Anbang stands out by treating each tubular steel tower as a critical link in connectivity, not just a product. What exactly goes into that precision, and why does it matter for the networks we rely on daily? The answer challenges common assumptions about where quality truly begins.
The Engineering Behind Precision Tubular Towers
Precision tubular towers rely on tight dimensional control at every stage, from raw coil slitting to final seam welding. The process begins with high-strength steel strip that is leveled and edge-milled to within a few hundredths of a millimeter. This pre-work eliminates the inconsistencies that would otherwise accumulate when the strip is fed into a series of forming rolls. Each roll set gradually curves the flat strip into a closed cylinder, with the final pass applying pressure precisely at the weld point to avoid any misalignment. Manufacturers often switch between high-frequency induction welding and submerged arc welding depending on plate thickness, because each method introduces different heat-affected zones that can alter the tower's fatigue life.
Beyond geometric accuracy, the engineering focus shifts to residual stress management. A tubular tower section may be over ten meters long, yet it must keep a straightness tolerance of less than one millimeter per meter after galvanizing. Hot-dip galvanizing adds a protective zinc layer, but it also introduces thermal distortion. To counter this, some fabricators apply a controlled air cooling sequence that normalizes the temperature gradient across the tube's circumference. Additionally, internal longitudinal stiffeners are positioned not just for buckling resistance but to redistribute welding-induced stresses away from the most highly loaded regions near door openings and flange connections.
Field assembly adds another layer of precision. Instead of relying solely on oversized bolt holes, modern towers use machined flange faces with a specified surface roughness and a precise bolt preload pattern. This approach limits the angular misalignment between sections, which directly influences the tower's natural frequency and overall aerodynamic damping. Engineers often run full-scale modal tests on the first prototype of a new tower series, measuring vibration modes that cannot be fully captured by finite element models alone. The data feeds back into the manufacturing tolerances, ensuring every subsequent tower behaves predictably under turbulent wind loads.
Custom OEM Solutions for Diverse Network Demands
Every network tells a different story. Some run lean and quiet in a single office, while others sprawl across factories, branch locations, or remote field sites with radically different bandwidth, latency, and reliability requirements. Our custom OEM approach begins by listening to that story, not by assuming a one-size-fits-all product. We work directly with your engineering and procurement teams to translate real-world operating conditions into hardware and software configurations that fit without costly over-engineering or risky shortcuts.
From port density and power budgets to industrial temperature ranges and specialized uplink options, each unit can be tailored at the manufacturing stage. That means you receive equipment that already matches your deployment environment, whether it is a dust-prone warehouse, a temperature-swinging outdoor cabinet, or a tightly managed data center. We can also pre-load custom firmware builds, adjust default security profiles, and apply unique branding or labeling so the finished devices arrive ready for your specific rollout plan.
Because no two network demands are identical, our production lines support mixed-order flexibility without the long lead times typically associated with bespoke hardware. Small pilot batches, regional variants, and ongoing revisions are all treated as standard practice rather than exceptions. The result is a supply chain that moves at the speed of your project, delivering OEM solutions that feel less like off-the-shelf equipment and more like infrastructure built with your network's exact pressures in mind.
Material Integrity and Anti-Corrosion Treatments
Corrosion doesn't announce itself with a warning — it eats away at structural integrity long before visible rust appears. Effective material protection starts with selecting substrates that resist environmental attack, then layering on sacrificial coatings, galvanic barriers, or passivation treatments tailored to the specific exposure conditions. The goal isn't just to slow down degradation; it's to engineer a defense that adapts to thermal cycling, moisture ingress, and chemical contact without compromising the base metal's mechanical properties.
A common oversight is treating anti-corrosion as a one-time application rather than a system. For example, a zinc-rich primer alone won't hold up under constant salt spray unless paired with a compatible intermediate coat and a UV-stable topcoat. Similarly, stainless steel isn't universally immune — crevice corrosion can still occur in low-oxygen environments. That's why real-world material integrity relies on matching the treatment to the failure mode: cathodic protection for buried pipelines, anodizing for aluminum exposed to industrial atmospheres, or vapor-phase inhibitors for enclosed cavities.
Inspection and maintenance complete the loop. Even the best coating system underperforms if film thickness is inconsistent or surface prep skips abrasive blasting. Regular ultrasonic thickness measurements and electrochemical impedance spectroscopy reveal early coating breakdown before substrate loss becomes critical. Treating corrosion as an ongoing operational parameter — not an afterthought — keeps assets in service longer and avoids the hidden cost of sudden, unplanned replacements.
Streamlined Production from Cutting to Galvanizing
Raw steel enters the cutting line as full-length sections and is processed within hours, not days. Laser and plasma cutters work from shared nesting files, so offcuts are minimized before parts move to the adjacent forming station. Any dimensional checks happen at the cutter, which prevents misfits from reaching the galvanizing stage.
From forming, components travel by overhead conveyor to a pre-treatment bath that strips mill scale and surface oxides. The same conveyor then lowers them into the zinc kettle. Because the line speed is tied to material thickness, immersion time stays consistent, and the finished coating builds evenly across edges and weld zones.
Meeting Global Standards without Compromise
Every market has its own rulebook, but the underlying demand never changes: quality that holds up under scrutiny. Meeting global standards without compromise means refusing to treat certification as a box-ticking exercise. Instead, the product is shaped from day one around the strictest regional requirements—and then built to exceed them.
From CE marking to FCC, RoHS to REACH, each standard introduces constraints. The key is to treat those constraints as design inputs rather than afterthoughts. Materials, testing protocols, and documentation are all organized around the requirements ahead of time, so a product enters multiple markets without last-minute redesigns or quiet trade-offs.
This approach also changes the testing culture. Teams run continuous verification against the harshest thresholds on the horizon, not just the ones currently mandated. Global compliance becomes a natural byproduct of quality engineering, not a separate hurdle. Customers get the same core experience in every region, with no hidden downgrades or regional shortcuts.
Scaling Infrastructure with Reliable Tower Partners
Expanding coverage across a region rarely comes down to simply adding more steel. The terrain, local permitting, and existing utility access all shape where a site can actually go live. A tower partner that has already navigated county approvals, soil studies, and neighbor concerns removes a large part of the delay that typically stalls rollout timelines.
The difference between a partner and a vendor shows up after the first build. Reliable partners take responsibility for structural upgrades, grounding, backup power, and co-location coordination before those issues become network outages. Their field crews know which access roads wash out in heavy rain and which municipal inspectors require specific documentation, which keeps your deployment schedule from slipping.
When comparing options, past delivery records and local relationships matter more than the lowest bid. A partner with a track record of reinforcing towers for wind load or managing shared rooftop sites will lower long-term operating costs. That kind of dependability makes it possible to scale into new markets without building a separate infrastructure team from scratch.
FAQ
These towers are produced using automated welding lines and laser cutting, which keep dimensional tolerances within a few millimeters. The steel is typically high-strength low-alloy grades, and every batch undergoes ultrasonic and bend testing before assembly.
Yes, most OEM manufacturers have in-house engineering teams that work from your load calculations or site survey data. They adjust flange thickness, base plate dimensions, and section transitions to match specific wind zones and soil conditions.
Beyond routine visual checks, factories use coordinate measuring machines on flanges, magnetic particle inspection on welds, and trial assembly of random sections. Full traceability is maintained by stamping heat numbers on each segment.
Hot-dip galvanizing is standard, often to ISO 1461 or ASTM A123, with a minimum coating thickness of 85 microns. For aggressive environments, additional epoxy or polyurethane topcoats can be applied, and duplex systems are offered for areas with high salinity.
They are normally shipped as knockdown kits with each section nested or racked to reduce freight volume. All bolt holes are pre-drilled and match-marked, and assembly manuals plus torque specifications are included.
Depending on current production schedules and the complexity of the design, typical lead times range from 45 to 75 days after drawing approval and down payment. Urgent orders can sometimes be accelerated with overtime shifts.
Tubular towers have a smaller footprint, faster erection time, and a cleaner visual profile. They cost a bit more per ton than lattice structures, but lower foundation requirements and less land leasing often close the gap on total installed cost.
Many offer optional site advisory services, sending a welding or assembly supervisor for the first few towers. However, the standard contract covers fabrication, inspection, and loading at the factory; installation crews are usually arranged separately by the buyer.
Conclusion
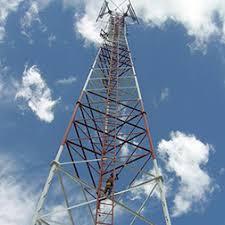
China’s tubular steel tower manufacturing has matured into a field where precision engineering and practical customization go hand in hand. Every tower begins with structural calculations based on actual deployment scenarios—wind speeds, soil conditions, seismic activity, and equipment loads—so the design remains efficient without sacrificing safety. Because OEM work is inherently flexible, tower heights, flange orientations, ladder placements, and platform layouts can be adjusted to match dense urban rooftop sites, suburban roadside installations, or remote mountain backbones. This adaptability extends to material choices: high-strength steel plates are sourced with full traceability and tested for tensile strength before fabrication. Once shaped and welded, towers receive hot-dip galvanizing or multi-layer anti-corrosion coatings that resist rust in coastal salt air, humid valleys, and heavily industrialized zones, keeping maintenance costs low over a service life measured in decades.
The production flow itself is designed to eliminate waste and inconsistency. Computer-controlled cutting, automated longitudinal and circumferential welding, and precision hole-drilling reduce human error, while each batch moves through dimensional checks and non-destructive testing before entering the galvanizing bath. Final inspection covers coating thickness, weld integrity, and section straightness. This disciplined process does not mean rigidity; factories regularly update jigs and tooling to handle custom OEM orders without slowing lead times. Compliance is treated as a baseline rather than a goal—most established manufacturers hold ISO 9001, ISO 3834, and telecom-specific certifications, and they routinely submit towers to full-scale load tests that mirror international standards. For network operators, partnering with these reliable Chinese OEMs means faster rollout for 4G, 5G, and microwave backhaul projects, with towers that are ready to carry heavier antennas and stronger network demands without re-engineering or field modification.
Contact Us
Contact Person: antor khan
Email: [email protected]
Tel/WhatsApp: 8613863903569
Website: https://www.qdabtower.com/